By Jason Doyle, Sr. Manager of Supply Chain
Supply chain disruptions have become a persistent challenge in medical device manufacturing. Global conflicts, shifting trade policies, logistics constraints, material shortages, and rising costs continue to create uncertainty across the industry.
For medical device manufacturers, these challenges can affect development timelines, validation activities, production schedules, and speed to market.
While external factors can’t always be predicted or controlled, the right manufacturing partner can help customers navigate uncertainty with greater confidence.
At Innovize, supply chain risk management is built into our process. Our focus is on maintaining visibility, strengthening supplier relationships, and providing customers with the information they need to make informed decisions throughout their programs.
Visibility Drives Preparedness
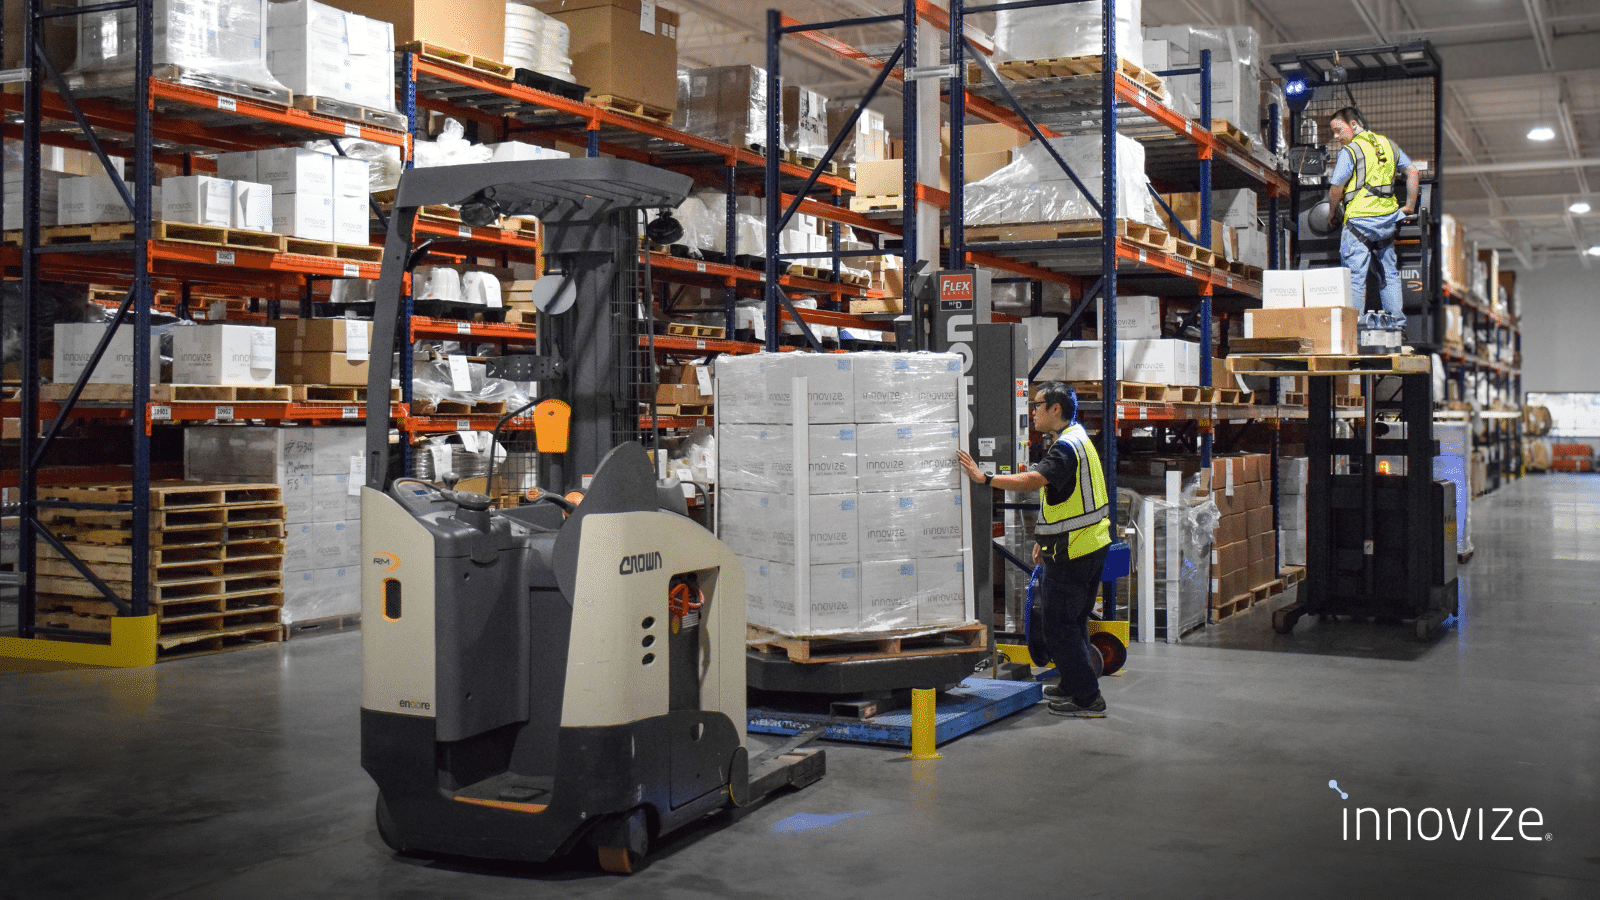
As a make-to-order manufacturer, Innovize does not rely on large inventories to mitigate risk. Instead, we prioritize visibility across every stage of the supply chain.
Our team continuously monitors supplier performance, open order status, material availability, and market conditions to identify potential risks early.
Forecasting also plays an important role. Through regular demand planning reviews, we compare booked business with projected customer needs to identify shifts in demand and emerging constraints. Forecasts are estimates, but they provide valuable insight that helps us prepare and communicate proactively.
Strong Supplier Relationships Create Stability
Long-term supplier relationships are central to our supply chain strategy.
We maintain close collaboration with our supplier network through ongoing communication, shared forecasts, and structured performance management. Supplier scorecards create accountability and support continuous improvement, while open communication helps identify potential disruptions before they impact customer programs.
These relationships also encourage suppliers to proactively share market insights, capacity constraints, and material availability updates, helping us respond more effectively when conditions change.
Supplier qualification and management are equally important. Our robust supplier management processes ensure customers benefit from a network of trusted partners who understand the quality, compliance, and performance requirements of medical device manufacturing.
Preparing for Future Challenges
Over the next several years, medical device manufacturers are likely to face continued pressure from geopolitical events, energy costs, freight and logistics challenges, and material price increases.
Materials such as resins, liners, packaging components, and specialty substrates may experience ongoing pricing pressure and variable lead times.
Innovize actively monitors these trends and works closely with suppliers and customers to understand potential impacts before they become critical issues.
Preparation helps reduce surprises and creates more opportunities to adapt.
Communication Builds Confidence
Clear, timely communication is one of the most effective tools for managing supply chain risk.
When potential challenges arise, we share information early so customers can evaluate options, adjust timelines, assess alternatives, and make decisions alongside our team.
This collaborative approach helps customers maintain momentum, even when market conditions change.
At Innovize, supply chain resilience is built on preparation, strong supplier partnerships, and transparent communication. Every decision is made with our customers’ programs, timelines, and long-term success in mind.